Complete Guide to Quality Inspection Methods Across the PCBA Manufacturing Process
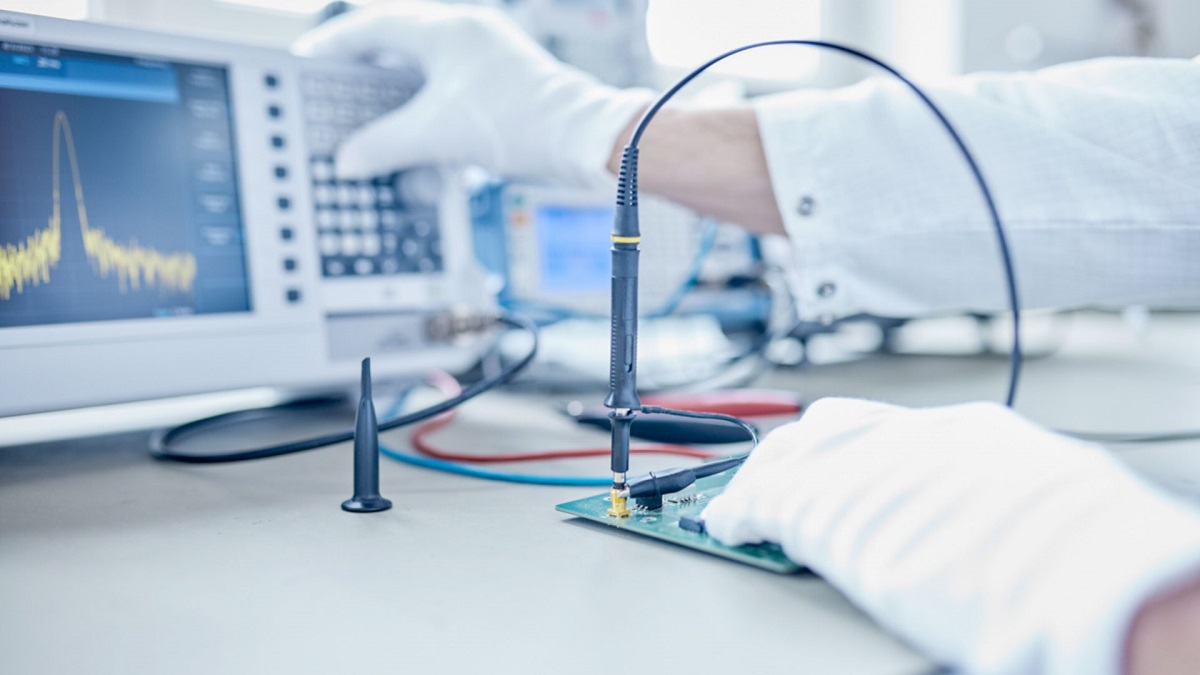
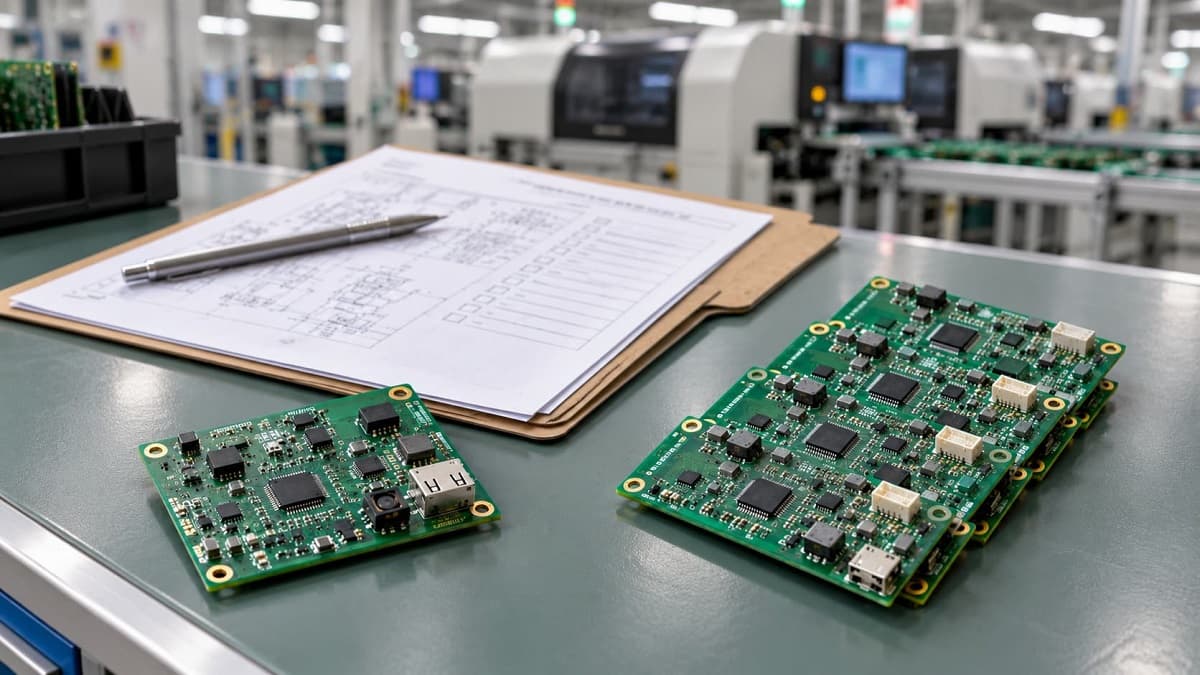
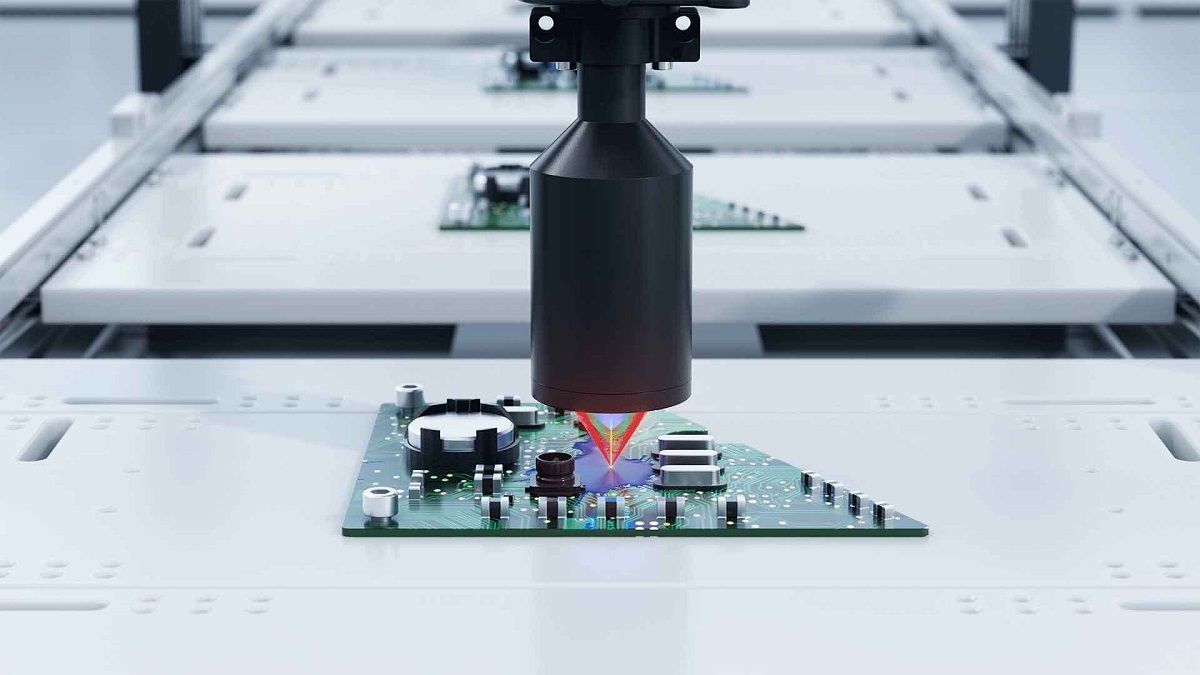
PCBA quality inspection should combine incoming material verification, controlled printing and placement, visual inspection, AOI, X-Ray for hidden joints, electrical testing, functional verification, and documented shipment release. The exact plan must reflect component packages, board design, application risk, and required defect coverage.
No single inspection method detects every PCBA defect.
Acceptance criteria must be agreed before production.
Buyers should verify records, traceability, calibration, and corrective action.
Inspect incoming PCBs and components
Verify identity, quantity, condition, date or lot codes, approved sources, PCB dimensions, finish, and required documentation. Segregate suspect material.
Control printing, placement, and soldering
Monitor solder paste, first-article setup, component orientation, placement, reflow profile, wave or selective soldering, and repair authorization.
Match inspection to defect visibility
Use visual inspection and AOI for visible placement and solder conditions. Use X-Ray when BGA, QFN, bottom-terminated, or other hidden connections create material risk.
Test electrical and functional behavior
Use continuity, flying-probe, ICT, programming, or functional tests according to accessible nodes, design maturity, volume, and operating requirements.
Review records before shipment release
Confirm results, nonconformance disposition, rework status, identification, quantity, packaging, and authorized release. See the full PCBA test process.
Is AOI enough for PCBA inspection?
No. AOI evaluates visible features but cannot prove hidden-joint integrity, electrical behavior, or product-level operation.
When should X-Ray inspection be used?
Use it when important solder connections are hidden or when process validation requires internal evidence. Sampling or full inspection should follow risk and agreement.
What evidence should a buyer request?
Request lot-linked inspection and test results, acceptance criteria, equipment and calibration records, operator authorization, nonconformance records, and release approval.
Acceptance, compliance, and core QC rules
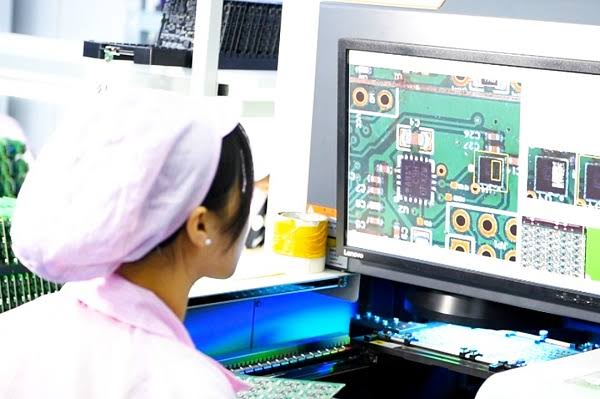
The IPC publication IPC-A-610, Acceptability of Electronic Assemblies establishes assembly acceptance criteria and product classes. IPC also describes J-STD-001 as requirements for soldered assemblies. Together, they support defining the applicable class, revision, and contractual criteria rather than accepting a vague claim of IPC compliance. Buyers should review the applicable PCBA inspection standards.
The ISO online text for ISO 9001 addresses identification, traceability where required, control of nonconforming outputs, and documented release. This supports retaining evidence that each lot passed defined controls; certification alone does not prove a specific board was tested.
Supplier quality capability evaluation
Ask the supplier to map each major defect to a prevention, inspection, or test control. Then sample records from one real lot and verify serial or lot linkage, limits, results, failures, rework, retest, and approval. Review quality traceability rules before approving volume production.